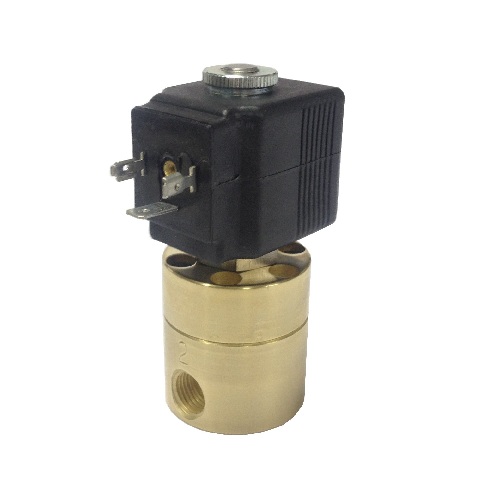

In chemical and pharmaceutical industries, where the handling of dangerous products is a constant, the security becomes a top priority. The risk of chemical leaks can have devastating environmental impacts, in addition to compromising the health of workers and generating high costs for companies. To mitigate these risks, pneumatic pumps emerge as a crucial solution, providing invisible security through its advanced sealing technology, essential for preventing leaks in critical environments.
In this article, we'll explore how pneumatic pumps are helping chemical plants prevent leaks and how their protective technology often goes unnoticed but plays a vital role in industrial safety.
What Are Pneumatic Pumps?
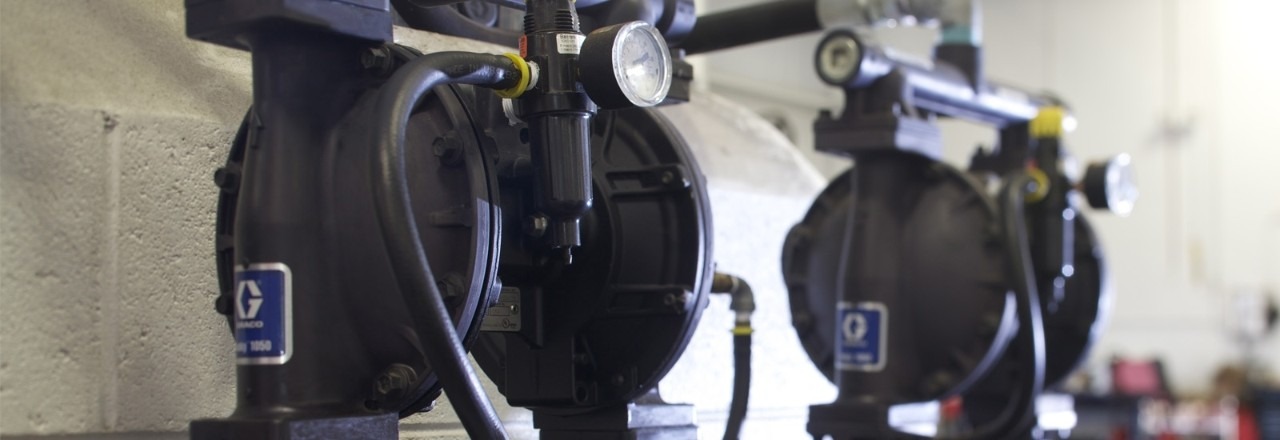
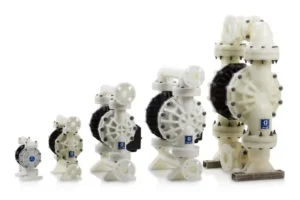
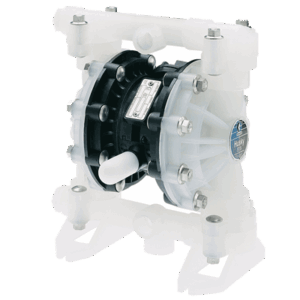
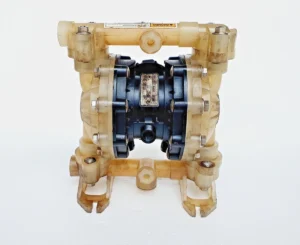
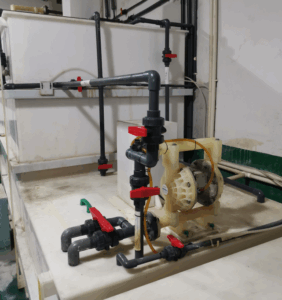
As pneumatic pumps are pumping systems powered by compressed air, capable of transferring liquids or other fluids efficiently and safely. Its operation is based on the alternating movement of membranes (diaphragms) or pistons, driven by air pressure. These devices are known for their robustness, versatility and ability to deal with viscous, corrosive and even abrasive fluids — common characteristics in chemical industries.
The great advantage of pneumatic pumps, especially in critical industrial applications, is their ability to operate with a double sealing or containment systems, designed to prevent leaks and protect operators and the environment from toxic substances.
How Do Pneumatic Pumps Prevent Leaks?
The main benefit of pneumatic pumps, when it comes to preventing leaks, is the Double sealing technology. Unlike conventional pumps, which can fail and result in leaks, pneumatic pumps use a sealing system that keeps the fluid inside the pump. bomba, preventing it from leaking into the external environment.
This sealing system is designed to be highly effective, providing additional security to the pumping system. If a failure occurs in one of the sealing elements, another containment system comes into action to ensure that the chemical is not released into the environment, protecting workers and the surrounding ecosystem.
Invisible Protection: The Technology That You Can’t See, But Is Always There
The concept of invisible protection refers to the ability of pneumatic pumps to prevent leaks and failures without requiring operators to notice an imminent problem. Often, these failures can occur internally in the sealing system or in the pump diaphragm itself, but thanks to double seal technology, the chemical never escapes the pump.
This type of technology is not often discussed, but its importance is vital to ensure the integrity of the industrial process and protect the health and well-being of operators. While preventative maintenance and attention to pump integrity are crucial, the sealing design of pneumatic pumps works continuously to prevent any failure from causing a leak, making this feature critical to daily operations.
Benefits for the Chemical and Pharmaceutical Industry
- Environmental and Legal Risk Prevention
In sectors such as the chemical and pharmaceutical industry, Prevention of leaks It is not only a matter of operational safety, but also of compliance with environmental regulations. Chemical leaks can result in Heavy fines, legal processes and irreparable damage to the company's reputation. With pneumatic pumps, companies can ensure that their processes meet the most stringent safety standards and avoid losses resulting from leaks.
- Workers Safety
Exposure to dangerous chemicals is a constant concern in chemical industries. The use of pneumatic pumps helps to reduce the risk of exposure to workers, as any leakage of harmful substances is contained within the sealing system, preventing toxic products from escaping into the work environment.
This additional level of safety is essential to protect the health of operators, who may be in direct contact with the pumps and fluids being pumped. With the invisible protection provided by pneumatic pumps, the risk of accidental exposure to dangerous products is significantly minimized.
- Greater operational efficiency and shorter inactivity time
Pneumatic pumps are famous for its reliability. Reduced system failures and leaks mean less downtime for maintenance and repairs. When the pumping system operates without interruptions, industrial processes can occur more efficiently, increasing the plant's productivity and profitability.
Furthermore, pneumatic pumps offer ease of installation and operation, making integration with existing industrial systems simpler and faster. The reliability and operational efficiency make these pumps an attractive solution for companies looking to reduce costs and improve their performance.
- Durability and reduction of maintenance costs
Pneumatic pumps are designed to operate for long periods, with less maintenance required. Its robust structure and advanced sealing technology guarantee a longer service life, reducing costs with repairs and replacement of parts. Additionally, the double sealing system helps prevent serious failures that could result in unexpected costs for emergency repairs or replacements.
The durability of pneumatic pumps is one of the main reasons why many maintenance engineers and purchasing managers consider this technology as a long-term investment.
How to choose the ideal pneumatic pump for your industry
When choosing a pneumatic pump for your plant, it is important to consider a few key factors:
- Construction material: To ensure resistance to corrosion and abrasion, it is crucial to opt for pumps made from materials such as stainless steel or resistant metal alloys, especially when dealing with aggressive chemicals.
- Flow capacity: Choose a pneumatic pump with the appropriate flow capacity for the needs of your operation. It is important to correctly size the pump to ensure optimal performance.
- Sealing technology: Check that the pump has an effective sealing system and offers an extra layer of protection against leaks. The double sealing system is an essential feature for critical environments.
- Ease of maintenance: Consider pumps that offer Facilitated Access for maintenance and repairs, as well as spare parts kits that simplify the process and reduce downtime.
Conclusion
As pneumatic pumps are fundamental to ensuring safety and efficiency in chemical industries, especially when it comes to preventing leaks of dangerous products. With their double seal technology and containment capacity, these pumps function as a invisible protection, ensuring that leaks do not compromise worker safety or cause serious environmental impacts.
Invest in pneumatic pumps not only improves operational efficiency, but also contributes to environmental compliance, reduced maintenance costs and protecting the health of employees. Therefore, if you want Protect your plant and avoid leaks, the solution lies in pneumatic pumps — a discreet technology, but essential for the safety and sustainability of industrial operations.