
Study: Optimization of the Operation of a Bomba Double Diaphragm Pneumatics and Monitoring Through a Pressure Transducer.
- SUMMARY
Compressed air pressure is a significantly variable quantity to long or poorly designed distribution networks. These variations can be determinant for the efficiency of equipment operation such as actuators, valves, pumps, etc. The project of this article was designed to control the pneumatic pressure of a Double diaphragm pumpallowing a continuity of work even in compressed air network pressure variations. The article also addresses other information on the components and aspects of monitoring through a pressure transducer.
- INTRODUCTION
In the automation of movements in the industry, energy can be used in different ways. Electricity in its traditional forms, hydraulic energy when the need for great efforts and pneumatic when we need moderate effort and large speeds, when the environment requires a higher degree of cleaning or when it is flammable or hostile.
Various air consumption in industrial plants, caused by machines and equipment that, sometimes consume more, now consumes less, make it impossible for compressed air availability in continuous flow of pressure and flow. Compressed air networks in industry in a common situation usually oscillate between 4 and 6 bar of pressure, but in high consumption or a long distance from the compressed air generator pressures can reach around 2 or 3 bar causing faults in pneumatic systems and/or productivity loss.
- Definitions of operation.
The system is based on reading and interpreting pressure by the pressure transducer that sends the information to Pascal-based programming software.
The transducer has a 0-10 bar input range with 0-10vcc output, as shown in the tables below.
| Range | Output | Range | Output | |
| 1 BAR | 1 vcc | 6 BAR | 6 vcc | |
| 2 BAR | 2 vcc | 7 BAR | 7 vcc | |
| 3 BAR | 3 vcc | 8 BAR | 8 vcc | |
| 4 BAR | 4 vcc | 9 BAR | 9 vcc | |
| 5 BAR | 5 vcc | 10 BAR | 10 vcc |
Figure 1.
Through the software the user enters the command data in the opening and closing pressures of the solenoid valve. With the opening of the valve the pressure flow enters the pressure multiplier (multiplication factor 2.0) that moves your pumping by raising the pressure until reaching the 2P pressure, as shown in the graph below.

Figure 2.
The pressure multiplied by the multiplier that can also be called booster moves to a compressed air accumulator with the following dimensions Ø125 x 450mm with volume capacity in liters of 557.77 liters to 10 bar bar.
Formula for volume calculation:
V1 = π. r². C
V1 = 3,1415. 62.5². 450
V1 = 5.522.167,9 mm²
V1 = 5,522,167.9 / 1,000,000 (mm³ / liters)
V1 = 55.22 liters
Volume calculation formula with pressure of 10 bar:
V2 = (P1 . V1)/ATM
V2 = (10. 55,22)/0,99
V2 = 557.77 liters with 10 bar
Being:
V1: AR volume
r: Reservoir
C: Reservoir length
V2: Pressurized volume
P1: Air pressure within the reservoir
ATM: Local atmospheric pressure.
Multiplied and monitored pressure can be used in various applications. During this article we will present some of these.
Pressure transducer
Pressure sensors are transducers that convert physical pressure into proportional electrical signal, as shown in the following figure.

As we have seen, in this project this signal will be treated by an electronic circuit and subsequently processed by the software on the computer.
This pressure transducer is calibrated from the factory, but depending on the need, it can be adjusted.
When a pressure is applied, the deflection of the diaphragm (sensor) leads to changes in resistance implanted according to the piezorestative effect (variation of electrical resistance as a function of applied force), thus a change in conductivity. Compression and dilation efforts in the semiconductor crystal are used to produce changes in the resistance of the connected piezoelectric plants as a bridge circuit, thus varying the bridge output voltage according to the sensitivity specified in the transducer transducer
There are several pressure transducer models, such as differential pressure transducers as well as more fragile models to work with low pressure and be used in instrumentation circuits that are not in contact with the industrial environment, such as medical equipment, for example.
Study: Optimization of operation of a double diaphragm pump.
In this case study the objective of the project is to maintain a peak pressure of the fluid outlet pneumatic pump greater than 50% of air pressure available on the network. Increasing the work efficiency of the equipment.
| (P) | (2p) | (PP) | |
| Network Pressure (Bar) | Multiplied Pressure (Bar) | Fluid peak pressure (bar) | Booster -free fluid pressure comparison |
| 0,5 | 1 | (-)¹ | (-)¹ |
| 1 | 2 | 1,5 | (-)¹ |
| 2 | 4 | 3,44 | 1,5 |
| 3 | 6 | 5 | 2,75 |
| 3,5 | 7 | 5,85 | 3 |
| 4 | (-)² | 3,44 |
Figure 4.
| (-) ¹ Pump does not operate. |
| (-) ² Maximum power pressure: 7 bar |
Detail of system components.
Compressed AR accumulator
The main function of this accumulator will be to store compressed air so that a main device or actuator can be feed, such as a pump, pneumatic hammer, clutch or pneumatic brake, painting pistols, etc. Both need an appropriate amount of pressure for their proper functioning. The accumulator is powered by a pressure multiplier and monitored by a pressure transmitter sensor. Accumulator Dimensions: Ø125 x 450mm with a capacity of 557.77 liters with 10 bar pressure in bar.
Pressure transmitter
The sensor signal signal will be monitored by the software that will determine the maximum and minimum pressure limit ranges for the operation of the consumer device. When there is low compressed air network pressure, the transmitter sensor sends a signal to the relay that closes the solenoid valve contact, causing it to open a passage, as record, and the air moves to the pressure multiplier, increasing it until it reaches the desired level and after it moves to the compressed air accumulator/tank. The pressure transmitter is an IT -TR Velki Range model of 0 -10 bar, output 0 -10 VCC with feed of 13 -28 VCC.
Pressure Multiplier or Booster
Once air passes through the solenoid valve it reaches the pressure multiplier cylinder, where the compressed air pressure that arrives is amplified as desired. This can be multiplied up to twice its initial value. The pressure multiplier is a VBA model from SMC Multiplication Factor 1.0 up to 2.0 and a flow of up to 1000 L/min.
Solenoid valve
Solenoid valve is responsible for opening and closing compressed air flow into the pressure multiplier, it is commanded by the relay signal that allows the start of the pneumatic system. It is a valve 2/2 via 1/2 '' Body Brass N.F. With a diaphragm in neoprene and solenoid coil 220V. ACL ITALY BRAND, E108DB12/C/10611.
Retention valve
Retention valve allows compressed air flow in one direction, always blocking the opposite flow. It is a 1/4 ″ valve with an internal sphere/spring system.
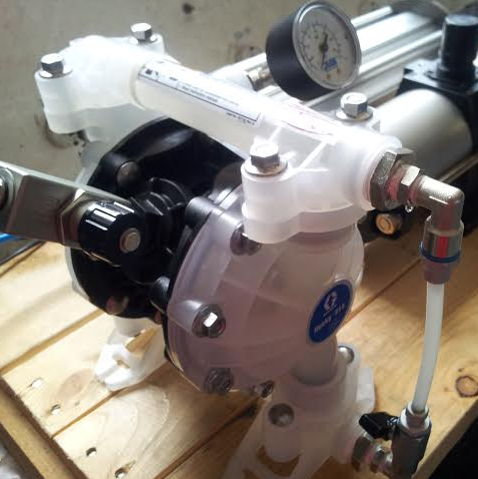
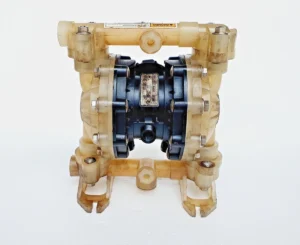
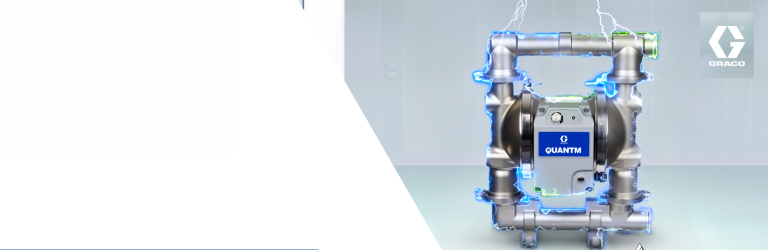
Double diaphragm pneumatic pump
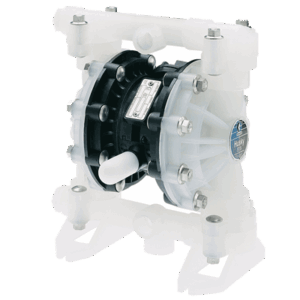
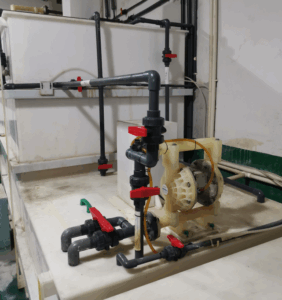
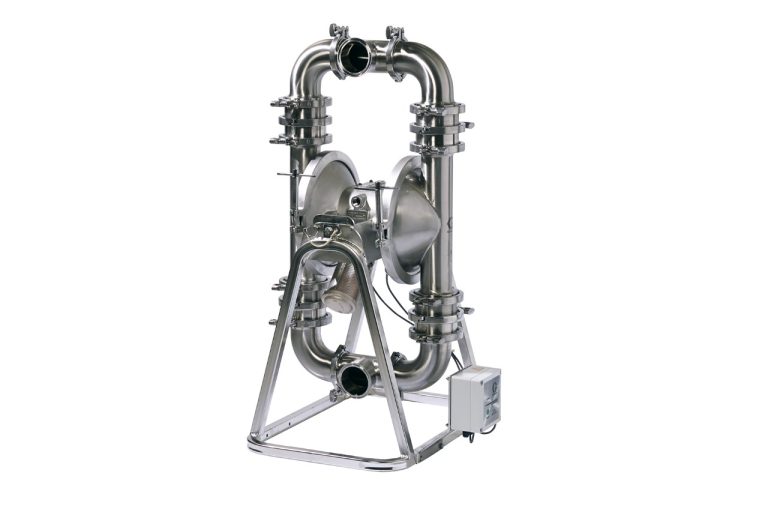
The central pump block has an air valve that directs the compressed air, initially pressurizing one of the diaphragms (camera B), which in turn drives the fluid in the camera in front of you (liquid chamber). Fluid is driven up due to the action of the sphere/seat sets, being directed to the exit through the collectors (manifolds), meanwhile the other diaphragm is pulled back by the axis that interconnects diaphragms, sucking the fluid into the other pumping chamber (Chamber A). When diaphragms complete its course, the valve pressurns the opposite diaphragm chamber, generating the same process already described above. The pump under study is a model pump Husky 515 Graco, 1/2 '. Polypropylene body, spheres, accents and diaphragm in Teflon, maximum flow of 61 l/min. Test fluid: water, viscosity 1 cps, 0% solids, atmospheric pressure 0.99 atm, output pressure and adjustable fluid input in the re-circulatory system.
Throttle
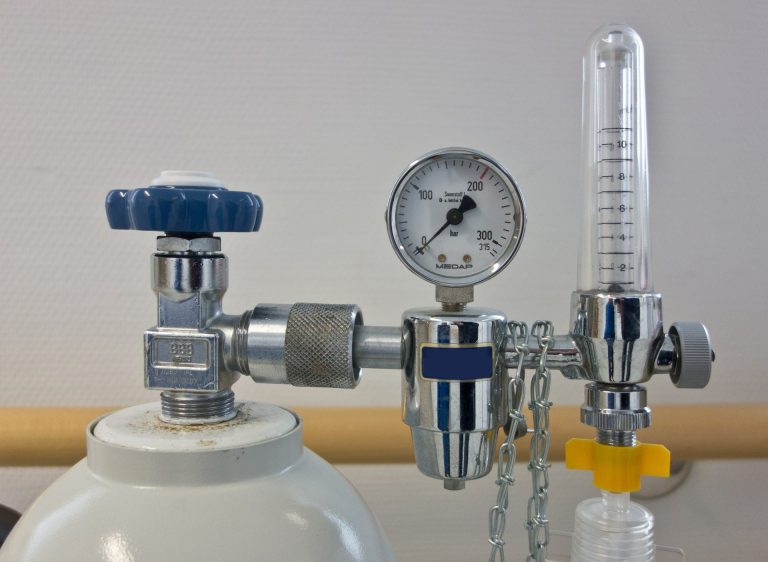
Pressure regulator is a device built to regulate the pressure of a fluid, usually having a higher and variable pressure in its input and providing a lower, reasonably stable pressure on its output.
In the scheme, there are two pressure regulators ¼ maximum pressure of 10 bar, with a maximum flow of 1100 liters at the pressure of 7 bar.
Electronic board
The plate that has been made for this project consists of a hardware that reads an analog signal (0 ~ 10V) and transforms into an electronic signal. This circuit is characterized as an A-D (analog to digital) converter. This analog value will be obtained from a pressure transducer, which will send voltage signals to the hardware, 1V - 1 bar, 1V - bar, 3V - 3 bar and so on.
When converting the signal issued by the transducer, it will be sent directly into binary to the parallel door.
Software Programming
Using Turbo Pascal software, and basic programming knowledge (see Figure 5 the programming lines), the control plate signal will be read. With this data on the screen, we made an automatic pressure control control from the hardware digital inputs, which will be arranged for 2 12V relay each triggered by transistors and 2 LEDs.

Figure 5 - Programming Lines.
Results Analysis.
After a series of tests using the devices, the transmitter operated with satisfactory response, monitoring the following measurements, as shown below:
| Media of pressure verified in the analog device (bar) | Transmitter sign (volt) |
| 0 | 0,58 |
| 1 | 1,55 |
| 2 | 2,48 |
| 3 | 3,55 |
| 4 | 4,55 |
| 5 | 5,55 |
| 6 | 6,55 |
| 7 | 7,55 |
| 8 | 8,58 |
| 9 | 9,5 |
| 10 | 10,58 |
Figure 6.
The multiplication factor (factor: 2.0) followed the input pressure with increased pressure as the following table:
| Multiplier input pressure (bar) | Pressure on the analog device verified at output (bar) | Pressure increase |
| 1 | 1,72 | 72,00% |
| 2 | 3,67 | 83,50% |
| 3 | 5,51 | 83,67% |
| 4 | 7,7 | 92,50% |
| 5 | 9,74 | 94,80% |
Figure 7.
Within the margin of error of the analog gauge and the paralax error we can consider that the components meet the goal effectively.
As shown in the next table, the bomba obtained the following result in conversion of pneumatic pressure to peak pressure from pumped fluid (PP)
| (P) | (2xp) | (PP) |
| Network Pressure (Bar) | Multiplied Pressure (Bar) | Fluid peak pressure (bar) |
| 2 | 3,67 | 3,33 |
| 2,5 | 4,59 | 4,13 |
| 3 | 5,51 | 5,17 |
Figure 8.
Other system applications.
The system can be perfectly used in other applications, such as:
Barbotine Mill Clutch: (Fig.: 9) With the pressure drop at levels such as 2 bar the mill clutch camera does not inflate enough to generate friction on the clutch canvas wall and the mill starts the “skating” movement the ribbons. This generates excessive wear.

Figure 9 - Barbotine mill.
Pneumatic brake (Fig.:10). Untilized in Barbotine Mill: The pneumatic brake is triggered by a piston that wraps the disc, when this piston has little pressure on the embolo it loses strength and as a consequence the brake loses the action. Occupational accidents may occur if the mill moves without proper care.

Figure 10 - Pneumatic brake.
Screen Tensioner (Fig.:11): Used to inflate a bladder serving as a surface for the manufacture of the screening screens used in the ceramic industry. When the bladder pressure is not suitable, the screen is flawed.

Figure 11 - Screen tensioners for screen printing.
Pneumatic hammer (Fig.:12): The hammer uses a minimal pressure to move your push pushing it against a high-tensile spring that soon after completing the course the air is expelled and the embolO returns with great force pushing the hammer. If the pressure is low the system does not work.

Figure 12 - Pneumatic hammer vibrator.
System Images


Always count on the double supplier. Contact us at (48) 3438-8484 or email vendas@duplacao.com.br And talk to our experts.