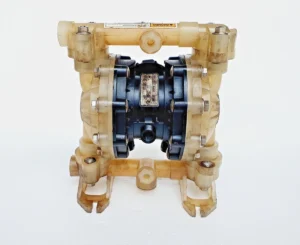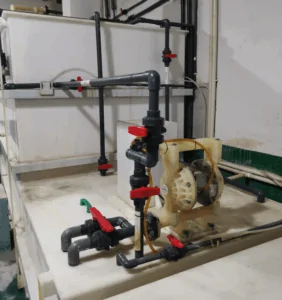

Pneumatic diaphragm pumps are widely used in industries from different segments due to its reliability, versatility and greater efficiency. One of these segments is the chemical industry, which can guarantee numerous benefits with the use of this equipment.
Common acquisition price lower when compared to other technologies and with the possibility of operating in different ways within the industry, pneumatic diaphragm pumps are gaining more and more space in the industrial environment. When we deal with the pumping of chemical fluids, there needs to be extra concern on the part of the industry, considering the risks that this type of material can bring.
Four benefits that the chemical industry can guarantee with the use of pneumatic diaphragm pumps
So that you understand how this equipment can be the best solution for the chemical industry, we have separated the main benefits of pneumatic diaphragm pumps that your industry can obtain with the use of this efficient and valuable equipment.
Dry and self -school pumping capacity
Dry pumping and the self-priming characteristic of pneumatic diaphragm pumps are the main advantages of this equipment. Thanks to these characteristics, your industry will be able to provide greater operational security and greater flexibility in the execution of numerous processes.
By being able to operate without the presence of liquid, especially in industries where this flow can be interrupted for any reason, it is possible to avoid damage to the equipment and bring more productivity and continuity to the processes. These pumps are also self-priming, which means there is no need to fill the cavity with fluid to start pumping. This advantage allows your industry to guarantee more productivity and efficiency, especially when there is a need to continually interrupt the process.
Versatility
Pneumatic diaphragm pumps can pump numerous types of fluids, from fine and volatile products to more abrasive and dangerous fluids. When we deal with chemical processes, it is important to have equipment that can handle different types of substances efficiently and with guaranteed safety.
This equipment has differentiated chemical resistance, being able to deal with bases, acids and solvents without deteriorating the equipment. To achieve this, these pumps are manufactured from different materials such as Teflon, stainless steel and polypropylene.
Another major difference is that pneumatic diaphragm pumps can transport noise with solid particles, without obstructing the equipment and blocking its operation. If it is necessary to pump fluids at extreme temperatures, pneumatic pumps are also an excellent option. For this reason, they are suitable for chemical processes that need to deal with this factor.
Robust and reliable design
A bomba Diaphragm pneumatics was developed with the aim of ensuring greater efficiency and safety for the industry. This guarantee begins with their operation without electricity, as these pumps only work with compressed air.
Its robust design allows it to be implemented in more extreme and adverse operations, considering variable pressure, exposure to the environment and corrosive fluids. One of the biggest advantages this equipment presents is that it operates with low pulsation, minimizing the risk of accidents, failures and mechanical wear.
Simplified maintenance and operating cost
As they are more robust equipment, pneumatic diaphragm pumps have a very simple maintenance process. Its project was developed to facilitate this process and with easily accessible components, allowing operators to replace parts without specific tools.
These factors allow for less downtime and, consequently, less impact on the operation of your chemical industry.
Pneumatic diaphragm pumps also have a low operating cost, being reliable and durable equipment. They do not require frequent repairs, reducing maintenance costs and, by using compressed air, it also saves energy.
We know that the pneumatic diaphragm pump has many other features that can facilitate and increase the productivity of your operation. In the case of chemical industries, the safety provided by this equipment is a great difference and can transform the routine of your business.
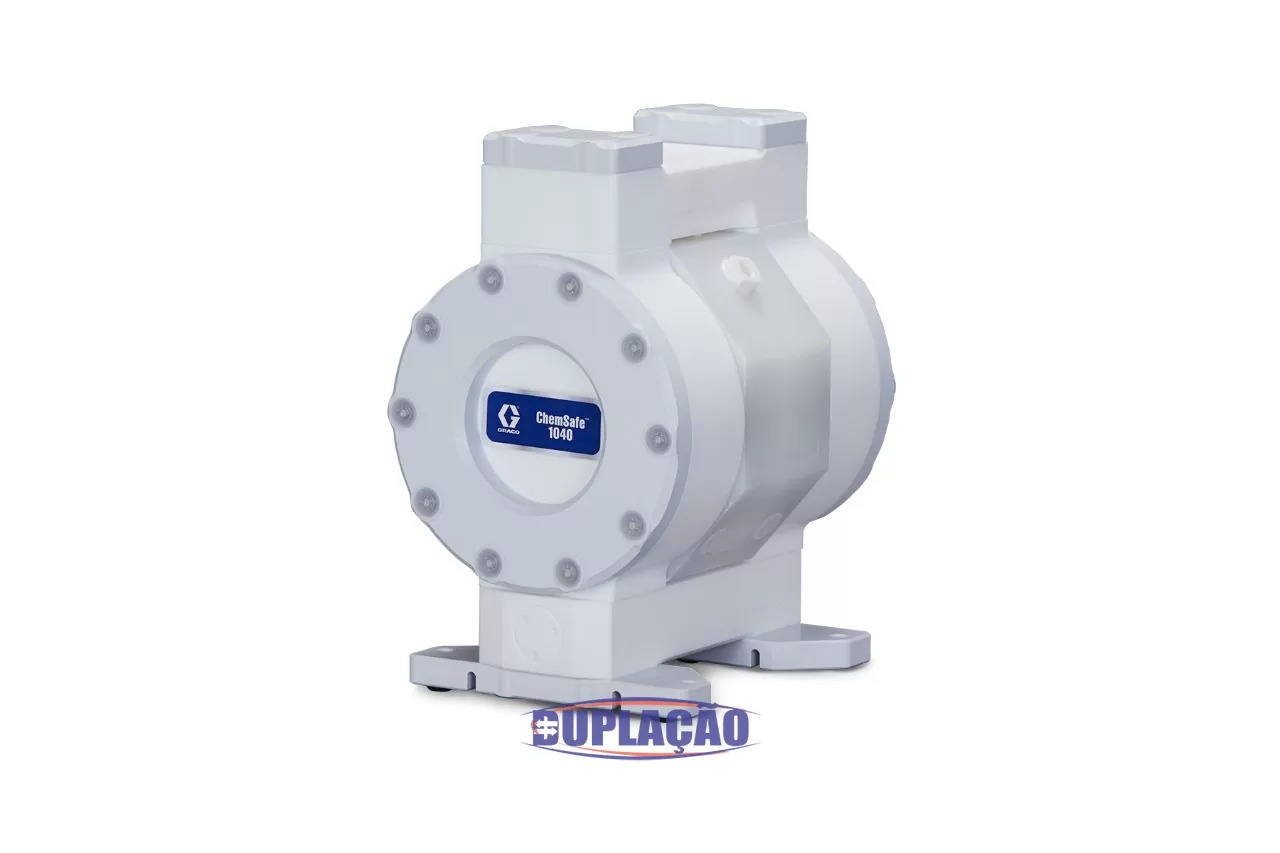
KNOW THE CHEMSAFE 1040 DOUBLE DIAPHRAGM PNEUMATIC PUMP – GRACO