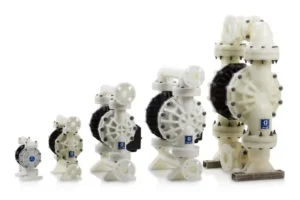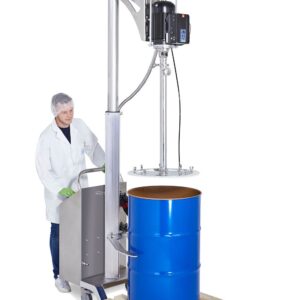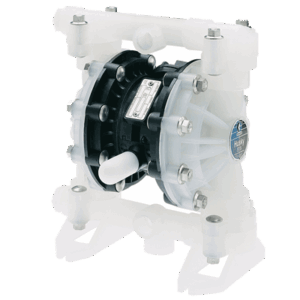

The mixing valve is an essential component in fluid automation and control systems. Its main function is to mix different fluids, ensuring that the correct proportion is maintained for specific applications. In this article, we will cover the characteristics, applications and benefits of mixing valves, highlighting their importance in the industry.
What is a Mixing Valve? – Definition and basic operation of the mixing valve.
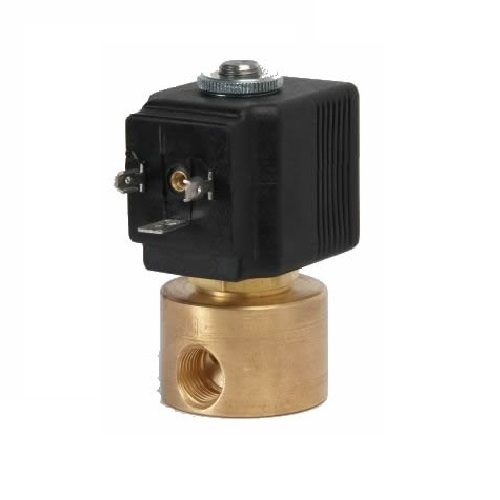
With mixing valve is a device used to combine two or more fluids in specific proportions. It is essential in industrial processes where the mixing of different substances is necessary to guarantee the quality of the final product.
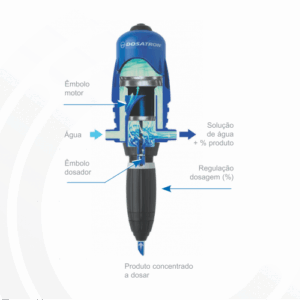
The basic operation of the mixing valve involves the flow regulation of each fluid entering the valve, allowing them to mix in a controlled manner.
When a fluid enters the valve, it is directed to a mixing chamber, where it combines with other fluids. Flow control is done through actuators that adjust the valve opening, ensuring that the correct proportion of each fluid is maintained.
Additionally, mixing valves can be equipped with sensors that monitor temperature and pressure, ensuring that operating conditions are ideal. This is crucial for industries that require precision, such as chemical and a alimony.
In summary, the mixing valve is a vital component that guarantees the efficiency and quality of industrial processes, allowing controlled mixing of fluids in various applications.
Applications of the Mixing Valve in Industry – Exploration of the various industries that use mixing valves, such as chemical, food and pharmaceutical.
With mixing valve It is widely used in various industries due to its ability to control the proportion of mixed fluids.
Na chemical industry, for example, these valves are essential for the production of chemical compounds, where precision in mixing reagents is crucial to guarantee the quality of the final product. Improper mixing can result in unwanted reactions or poor quality products.
Na food industry, mixing valves are used to combine ingredients in processes such as making sauces, beverages and dairy products. The ability to maintain product consistency and flavor is vital, and mixing valves help achieve this uniformity.
Also, in pharmaceutical, mixing valves play a key role in drug production. The mixing of active ingredients and excipients must be done precisely to ensure the effectiveness and safety of medicines. The automation and quality control provided by mixing valves helps meet stringent industry regulatory standards.
In short, mixing valves are indispensable in various industries, as they guarantee the efficiency of processes and the quality of final products.
Benefits of Using Mixing Valves – Advantages in terms of efficiency, quality control and cost reduction.
The use of mixing valves brings several significant benefits to industrial processes. One of the main benefits is the efficiency in fluid control. With the ability to mix different substances in exact proportions, mixing valves ensure that processes are carried out in an optimized way, reducing waste and improving productivity.
Another important aspect is the quality control. Precision in mixing ingredients is key to ensuring the final product meets the required standards. In industries such as food and pharmaceuticals, where quality is critical, mixing valves help maintain product consistency and homogeneity. This results in fewer variations and greater customer satisfaction.
Furthermore, mixing valves contribute to the cost reduction. By minimizing waste and improving process efficiency, companies can reduce operating costs. The automation provided by these valves also reduces the need for manual intervention, which can result in labor savings and reduced errors.
In summary, mixing valves are essential for improving efficiency, ensuring quality and reducing costs in various industrial sectors.
How to Choose the Ideal Mixing Valve – Criteria to consider when selecting the mixing valve for different applications.
Choosing the ideal mixing valve It is a crucial step to ensure the efficiency and effectiveness of industrial processes. There are several criteria that must be considered during this selection.
First, it is important to evaluate the Type of fluid that will be used. Different fluids have different properties, such as viscosity, temperature and pressure. The valve must be compatible with these characteristics to avoid failures and ensure adequate performance.
Another factor to consider is the mixing ratio. Depending on the application, it may be necessary to mix fluids in specific proportions. Therefore, the valve must be able to regulate the flow of each fluid precisely.
A operating pressure and temperature are also fundamental aspects. The valve must be able to withstand operating conditions without compromising its integrity. This is especially important in industries such as chemicals and pharmaceuticals, where conditions can be extreme.
In addition, the ease of maintenance must be considered. Valves that are easy to clean and maintain tend to have a longer lifespan and operate more efficiently.
Finally, it is essential to consider the total cost of ownership, which includes not only the purchase price, but also operating and maintenance costs over time. Evaluating all of these criteria will help ensure that the mixing valve you choose meets your specific application needs.