
Challenge: Transfer flammable and potentially dangerous aromatic solvents during the recovery process. The operation required equipment that guaranteed maximum safety, efficiency and reliability, minimizing the risks of fire and explosion.
The Scenario
The aromatic solvent recovery process is fundamental to sustainability and operational efficiency in industries that use these compounds, such as paints, chemicals and coatings. However, the volatile and flammable nature of these liquids poses a significant risk. Pumping these materials requires a solution that does not generate sparks or excessive heat, is resistant to aggressive chemical components and guarantees a continuous flow to avoid interruptions in production.
The Solution
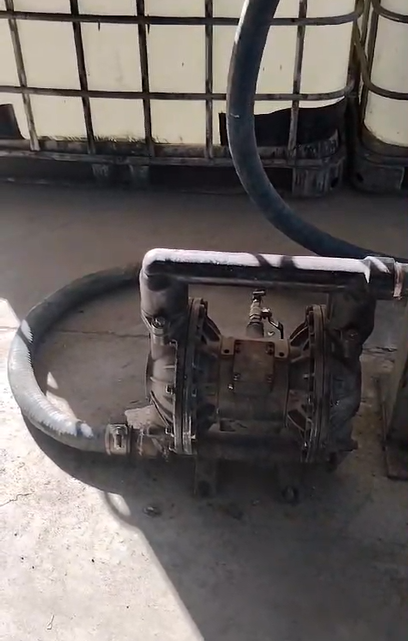
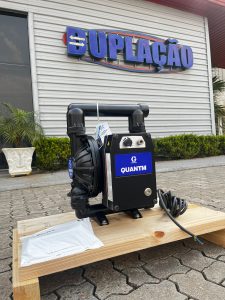
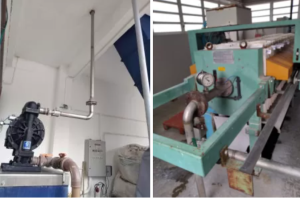
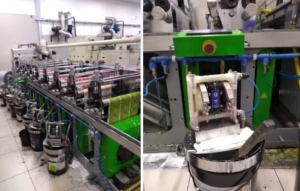
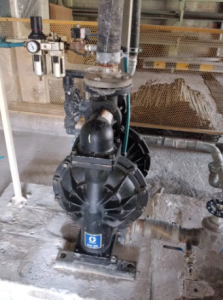
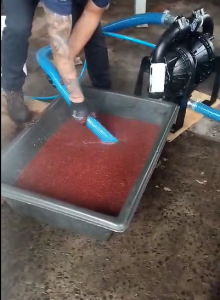
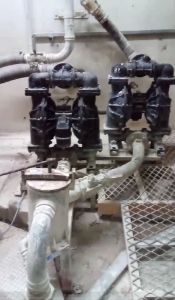
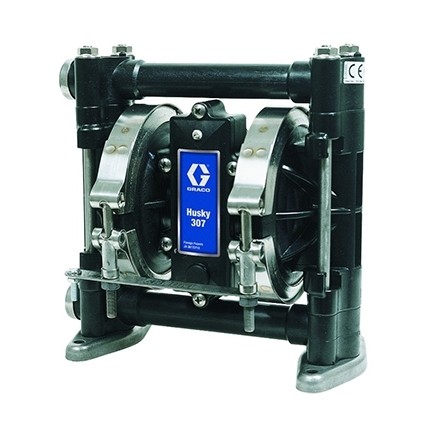
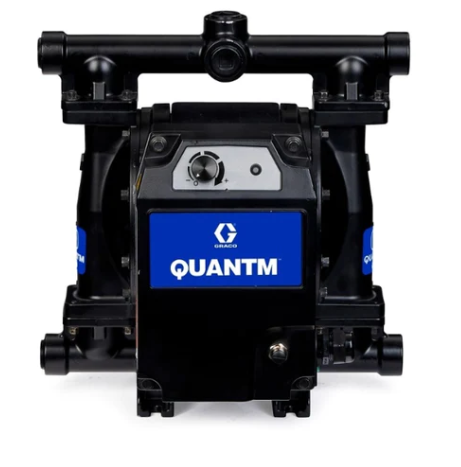
To meet these critical requirements, the pneumatic diaphragm pump was selected and implemented Graco Husky 2150. In the video, the pump is in full operation, connected to an IBC (Intermediate Bulk Container), which is a standard container for liquids. The features of the Husky 2150 were the ideal choice for the challenge:
- Intrinsic Safety for Flammable Fluids: The Graco Husky 2150 pump operates using compressed air, completely eliminating the need for electrical power in the pumping unit. This removes the risk of sparks, making it ideal and safe for use in hazardous areas and environments with solvent vapors, such as the recovery process.
- Handling Chemically Aggressive Fluids: The pump is designed to handle a wide variety of liquids, including aromatic solvents that can be corrosive to other types of pumps. Its robust construction with compatible materials ensures durability and consistent performance.
- Efficiency and Reliability: The low-maintenance design of the Graco Husky 2150 pump ensures continuous operation without unexpected downtime. This is vital for the solvent recovery process, where the constant flow of material contributes to optimization and productivity.
- Versatility and Ease of Installation: The video shows the pump installed in a simple and direct way, connected by hoses to the IBC. Its ease of installation and handling makes it a practical solution for transferring liquids between different containers and stages of the process.
Results and Benefits
Adopting the Graco Husky 2150 pump in the solvent recovery process resulted in significant gains:
- Increased Operational Security: The main benefit was the increased level of security. The absence of electrical components in the transfer area eliminated the risk of ignition, protecting the team and the plant.
- Improved Process Efficiency: A bomba assegurou um fluxo contínuo e confiável, reduzindo o tempo de bombeamento e minimizando interrupções na produção.
- Maintenance Cost Reduction: A robustez do equipamento e sua resistência aos solventes diminuíram a necessidade de reparos e substituição de peças, resultando em economia de custos a longo prazo.
- Contribuição para a Sustentabilidade: Ao garantir a transferência segura e eficiente dos solventes a serem recuperados, a bomba desempenha um papel crucial na redução de resíduos e no aumento da reutilização de materiais.
Conclusion
A bomba de diafragma pneumática Graco Husky 2150 provou ser a solução ideal para os desafios da recuperação de solventes aromáticos. Sua tecnologia intrinsecamente segura, combinada com alta eficiência e durabilidade, faz dela um equipamento indispensável para indústrias que buscam otimizar seus processos, proteger seus ativos e priorizar a segurança de seus colaboradores.