
The manufacturing and treatment process within the industry can utilize a wide variety of chemicals. These products are made up of different chemical components, ranging from simple and environmentally friendly compounds to products with highly toxic chemical properties, so it is necessary to have appropriate equipment that is chemically incompatible with their composition.
Industries dealing with chemicals face a variety of environmental, safety and flow challenges, which can include:
Leaks of chemical products that can cause serious consequences for the health of employees and the environment;
Loss of revenue due to leakage of expensive chemicals;
Limited useful life of the equipment used, which can cause the industry to face high replacement and maintenance costs.
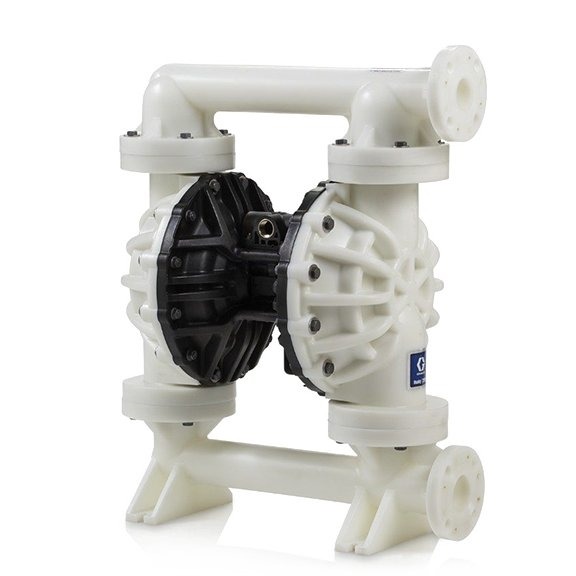
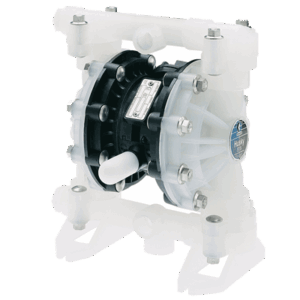
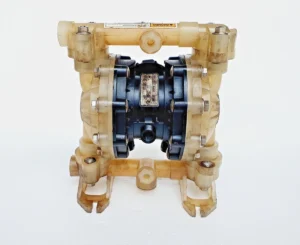
Pneumatic diaphragm pumps could be the right choice for this sector
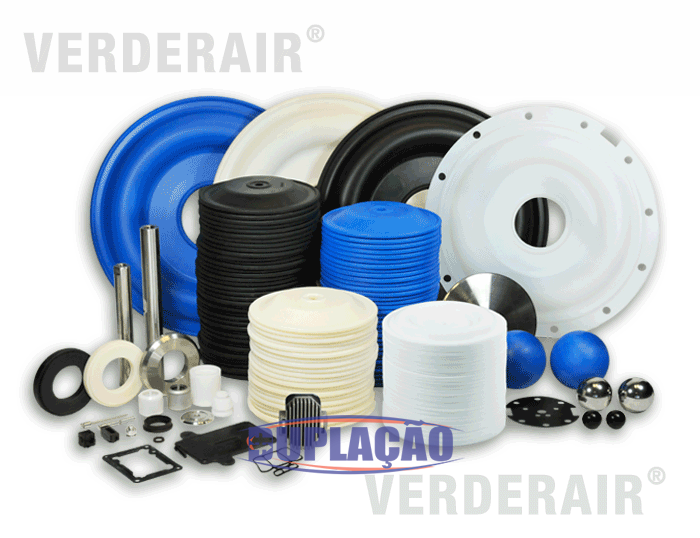
Pneumatic diaphragm pumps are ideal equipment for industries that manufacture and deal with chemical products, delivering durability, reliability and resistance in hostile environments. Being made up of a wide variety of materials, these pumps provide flexible configurations for your operation, dealing with varied chemicals and different viscosities, dealing with thicker and more abrasive fluids.
With a robust construction and bolt-on design, these pumps can, with minimal air consumption, offer maximum flows with reliable and productive performance, even in the most challenging operations in the chemical industry. These pumps have a simple and easy installation and have different port sizes, meaning they can be used conveniently and without the need for constant maintenance.
Most common applications of bomba diaphragm pneumatics:
Displacement processing of abrasive materials. such as polymers, plastics, glues, pesticides, adhesives, ammonia, coatings, petrochemicals, additives, fertilizers, lubricants and many others;
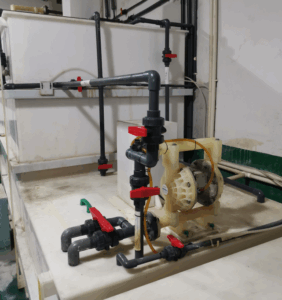
Safe transfer and mixing: transferring chemicals can be high risk and expensive, so these pumps can deliver practicality and performance for this application.
Wastewater, septic tanks and wells, filter presses, drainage, water treatment area, sludge removal and etc.
Application in aggressive environmental conditions, explosive atmospheres, corrosive environments, high temperatures, high suction lift requirements, dirty ambient air and more.
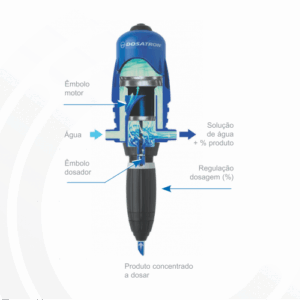
Dosage: due to their high efficiency, these pumps are able to deliver uniformity in all injection batch cycles.
Click here and see the perfect pump for the chemical industry!